MasterValve: The Innovation That Brews Success in Coffee Packaging
For years, the coffee packaging industry has faced a common challenge: balancing the need for airtight freshness with the demand for efficient and sustainable production. At Masterpack, we’ve always believed that innovation is the key to solving such challenges, and our patented MasterValve is a testament to that philosophy.
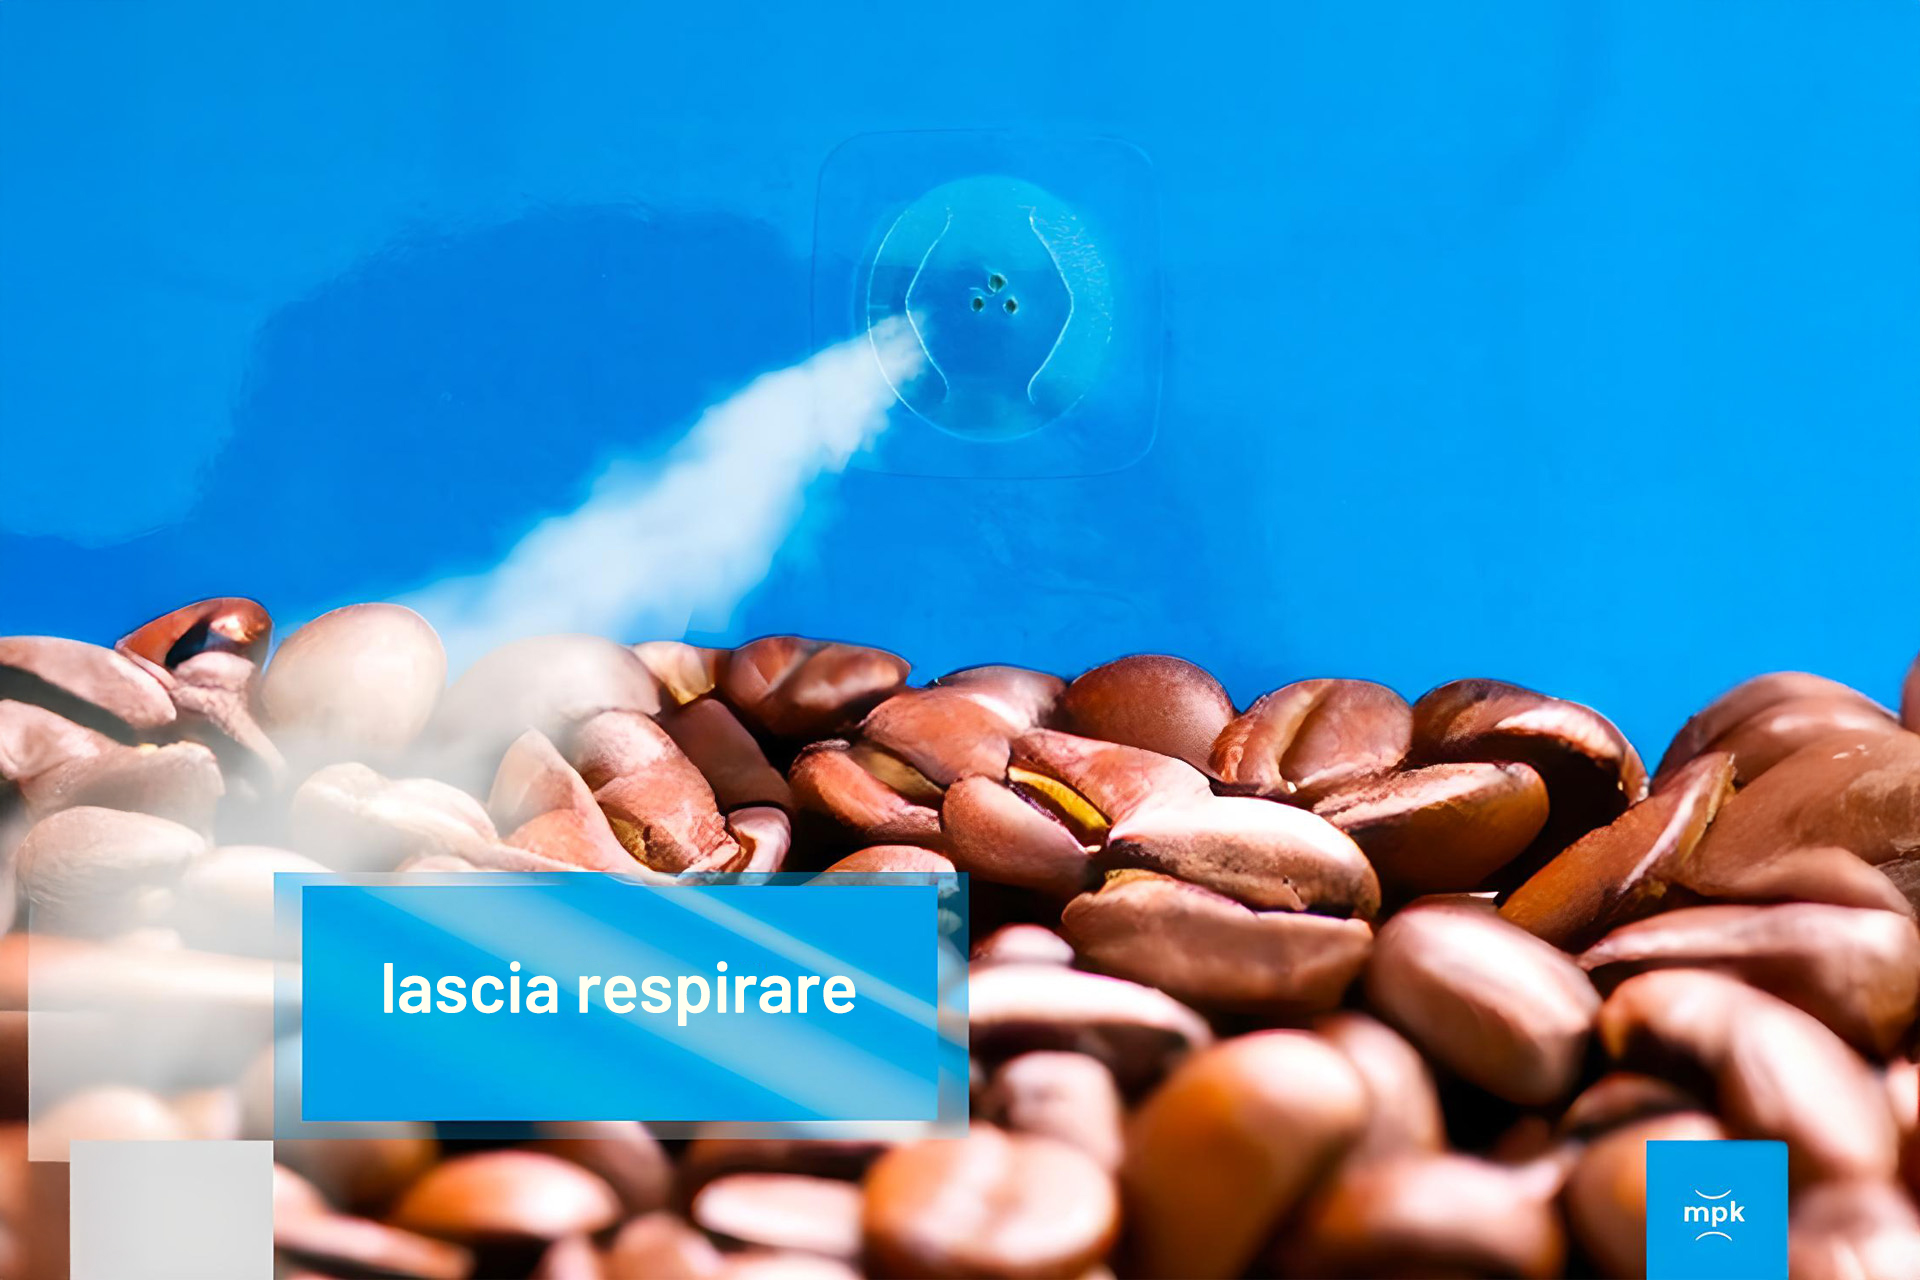
Initially developed in 2010 as a valve for microwave cooking, we’ve since perfected MasterValve to become the ultimate solution for coffee packaging. Unlike the older, outdated button valves that often create production bottlenecks, our system has the unique advantage of being pre-applied to the reel. This simple but brilliant design significantly increases the speed of packaging machines, allowing for a faster, smoother, and more efficient production cycle.
The benefits of MasterValve are a “jackpot” from every point of view. It’s a practical solution that streamlines your production process. It’s economic, offering a much lower cost than older systems. Most importantly, it’s an ecological triumph. The packaging can be certified as entirely recyclable, a crucial advantage in a global market that is increasingly devoted to green solutions and the elimination of waste. By ensuring the longevity of coffee freshness, our valve also plays a role in eliminating food waste.
The coffee roasting industry has embraced MasterValve as a true revolution. With three international patents, it represents a core part of our commitment to pushing the boundaries of packaging technology. We at Masterpack are incredibly proud of this invention and its continued success.